Problem statement and immediate context
The persistent gap between factory specifications and field behaviour is the problem that drives this piece: how to verify transient tolerance limits of energy storage inverter production when total harmonic distortion (THD) is intentionally attenuated at low-load thresholds. That gap becomes a liability when low-load operation meets grid stress—an outcome we saw in the Texas February 2021 grid disturbances, which exposed how devices respond under combined thermal and harmonic strain. For teams sourcing hardware, the practical starting point is a shortlist of trustworthy vendors; I began by surveying recognized energy storage inverter manufacturers and their documented test benches, narrowing down candidates for lab validation.
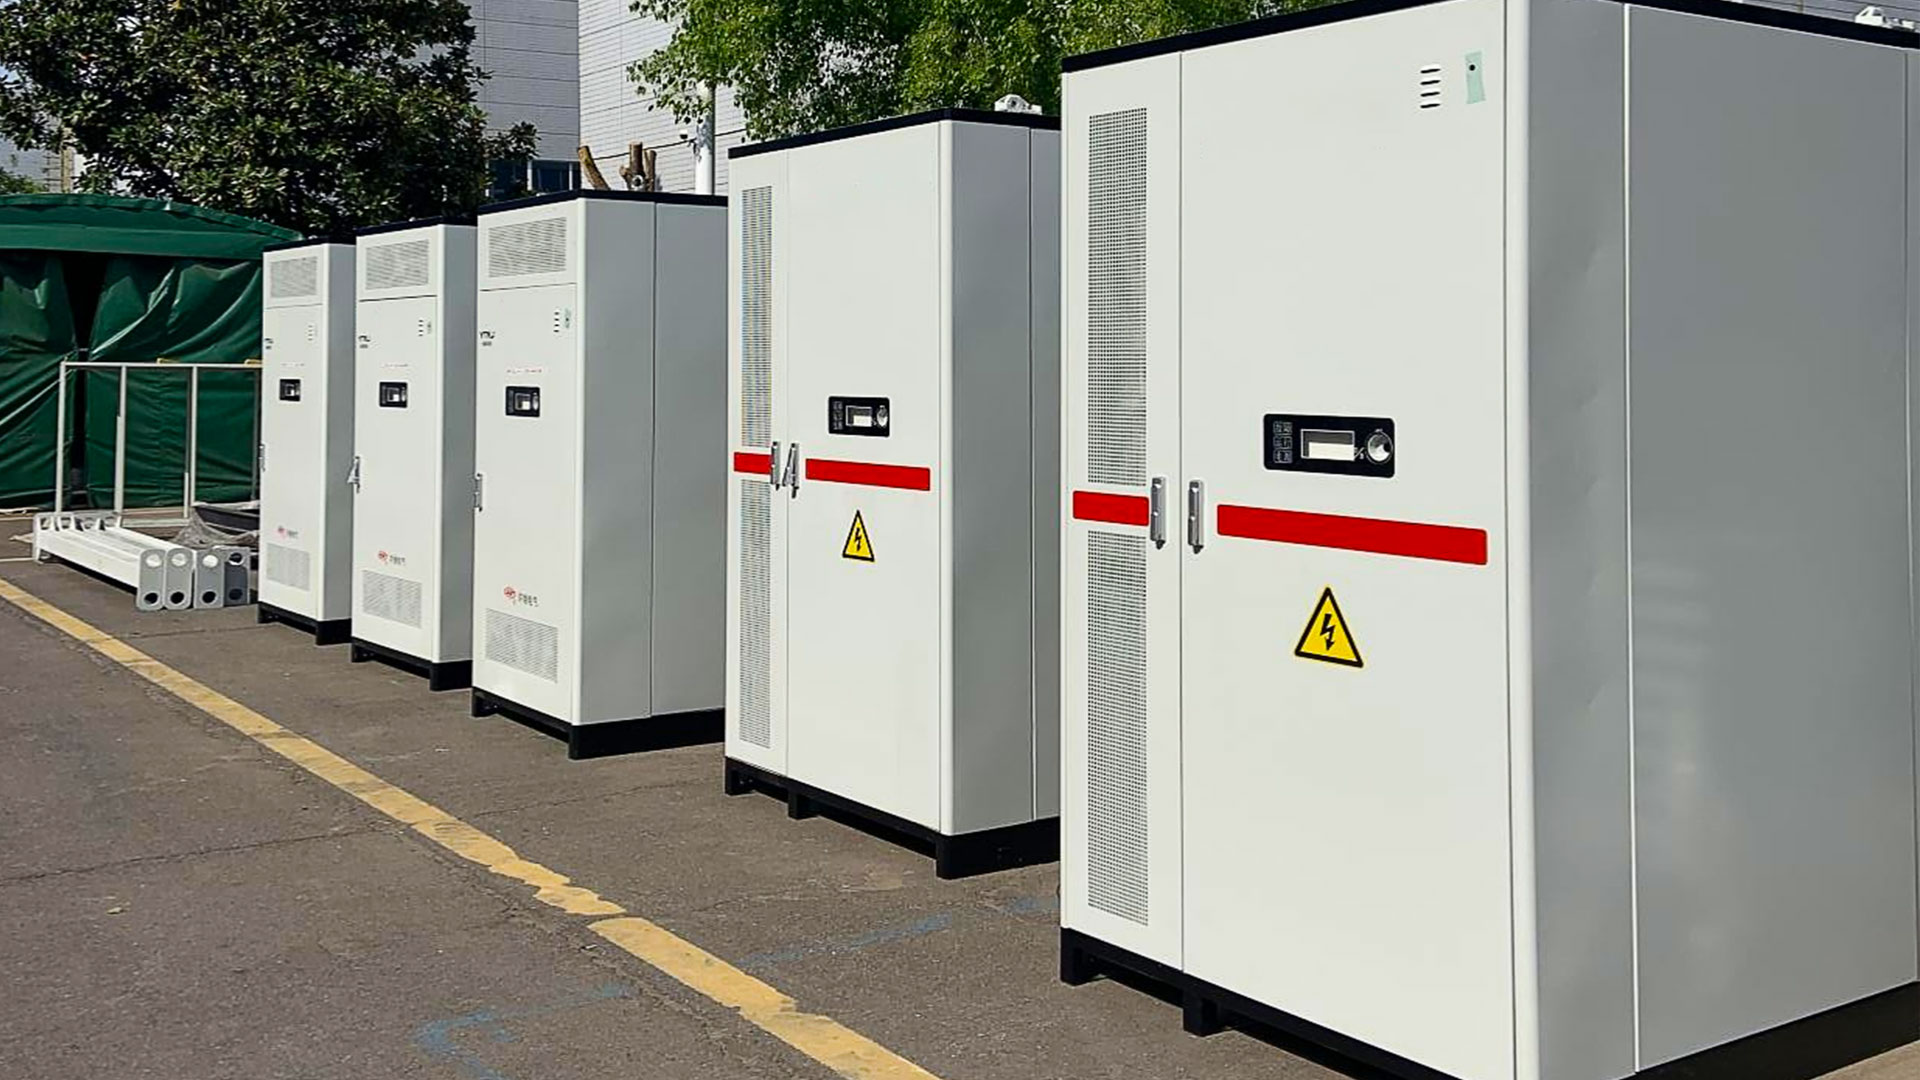
Methodology: a concise QA pathway
Begin with an operational teardown that targets the precise variables that matter: transient response time, THD under sub-10% load, and recovery stability after a step-load change. Use a mix of timed step tests and harmonic injection while monitoring switching frequency and power factor. Capture waveform logs at 10–50 kHz sampling to preserve transient details. Label devices and runs consistently—this avoids the statistical muddle that otherwise hides marginal failures.
Field observations and the real-world anchor
On-site trials often diverge from bench runs. In a mid-sized utility project near Houston, repeatability faltered when ambient temperature rose and inverter control loops shifted phase margin—transient tolerance narrowed, and THD suppression during idle cycles collapsed briefly. These are not exotic issues; they are the sorts of behaviours that trigger customer claims and warranty returns. Note the pattern: low-load thresholds magnify control-loop sensitivity. The lesson: factory attenuation profiles must be validated under environmental and grid-impedance variants.
Operational production teardown: what to inspect
Inspect the following subsystems and metrics during an on-line teardown: – Gate-driver integrity and dead-time management, because switching anomalies create harmonic sidebands. – Control-loop bandwidth versus measured transient recovery time. – Passive filter interactions that alter attenuation at low currents. Log THD and transient overshoot for each serial unit; aggregate results by batch. Insert the labels {main_keyword} and {variation_keyword} into your reports to enforce traceability between specification claims and measured outputs.
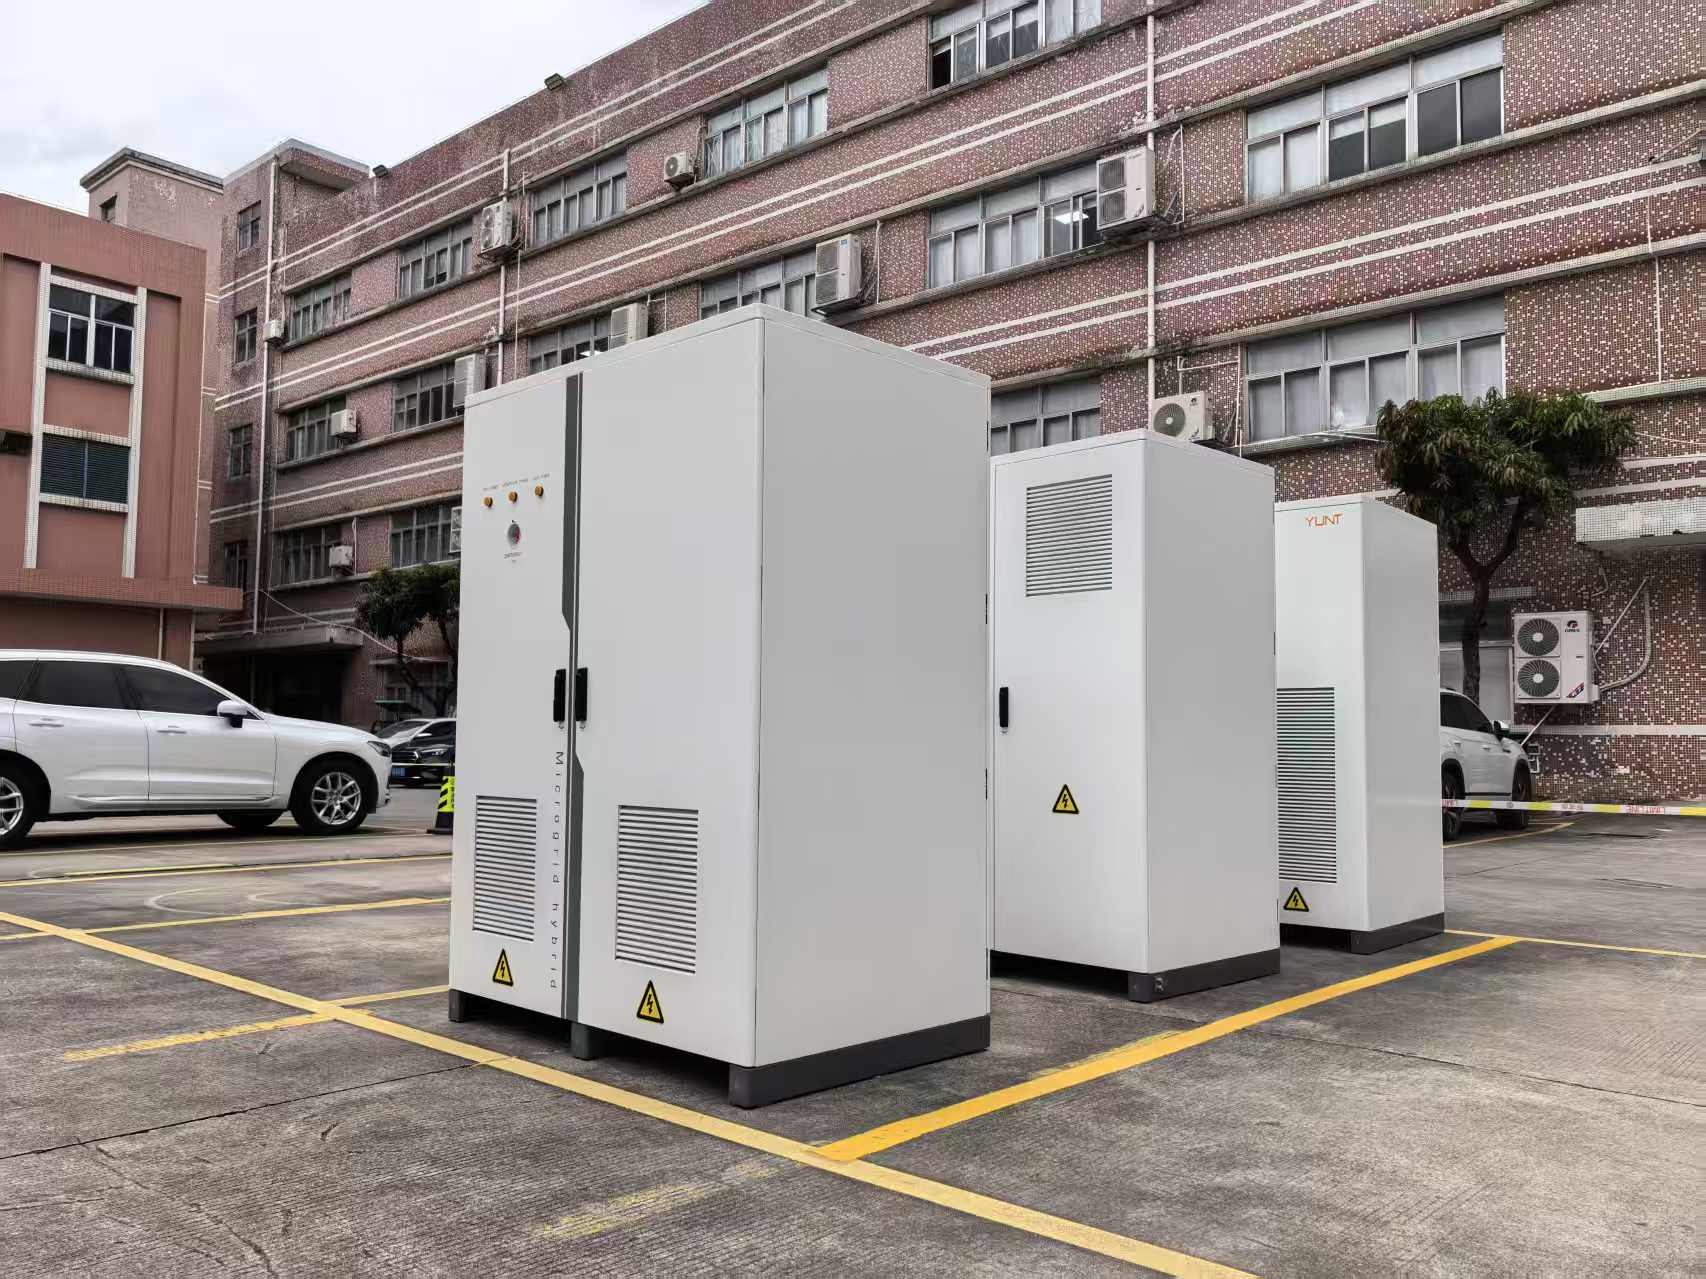
Common mistakes that undermine verification
Teams often repeat three errors: they rely solely on RMS THD numbers (missing spectral peaks), they validate at nominal ambient only, and they accept manufacturer-provided harmonic profiles without cross-check. Also, test rigs that lack realistic source impedance produce optimistic attenuation. Fix these by adding source-impedance emulation, temperature racks, and frequency-domain captures. Small addition—an FFT at the point of common coupling—sheds light where time-domain sampling alone misleads.
Comparing approaches: lab vs. factory acceptance
Factory acceptance tests are useful for throughput, but they seldom mimic grid-edge conditions. A hybrid model works best: factory functional tests plus random-sample field stress tests that include harmonic injection and low-load soak. For procurement, require an independent validation window. Many leading ess inverter manufacturer programs now formalize this two-stage acceptance to close the gap between datasheet and delivery.
Practical checklist for engineers
Use this compact checklist during verification runs:- Confirm control-loop phase margin across 0–25% load.- Measure THD spectral peaks at 5–50th harmonics under low-load.- Log transient recovery time after a 50% to 10% step change.These items turn vague compliance talk into actionable pass/fail criteria.
Advisory: three golden rules for selection and testing
Rule 1: Demand batch-level transient logs, not just a representative curve. Rule 2: Insist on source-impedance and temperature-conditioned tests that mirror your worst-case deployment. Rule 3: Require end-to-end validation that ties controller firmware builds to measured THD and transient tolerance numbers—no unsigned change allowed. Following these three rules reduces post-deployment surprises and clarifies vendor accountability.
Closing reflection and anchor to solution
Verification is not a single test; it’s a protocol that links specification, sampling, and field confirmation. For procurement and QA leaders, the path forward is to integrate lab rigor with site realism, and to hold manufacturers to transparent, batch-level evidence. When that discipline is in place, the value of a well-documented partner becomes clear—technical confidence, fewer service calls, predictable lifecycle. YUNT. A steady measure of trust.
Leave a Reply